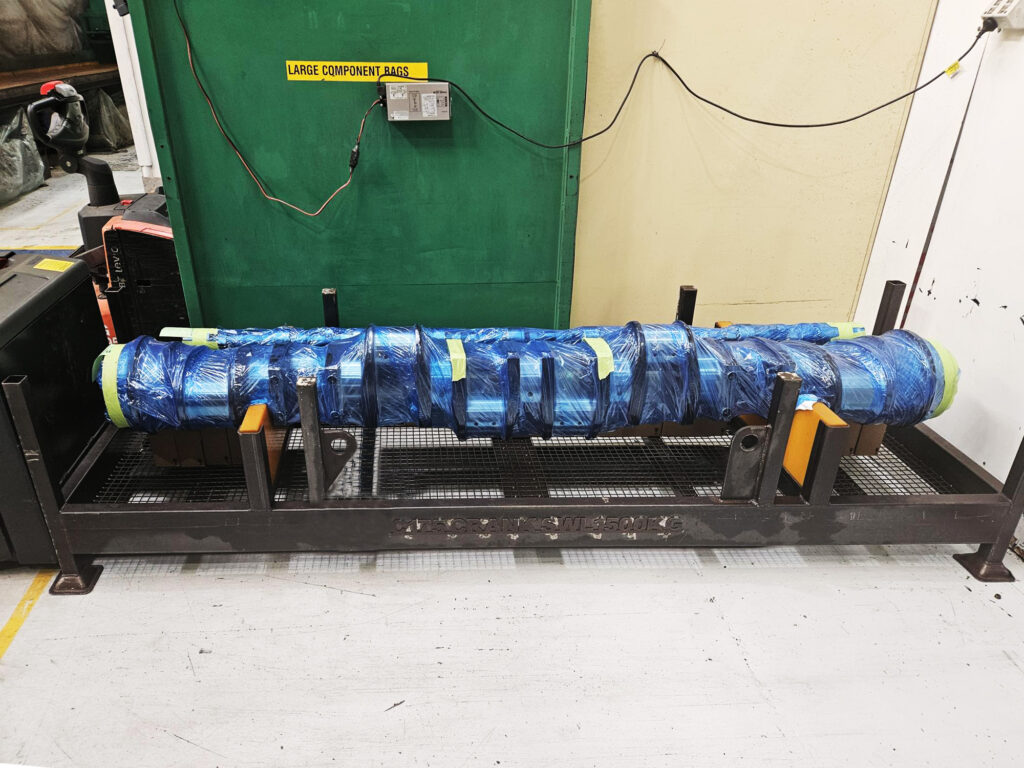
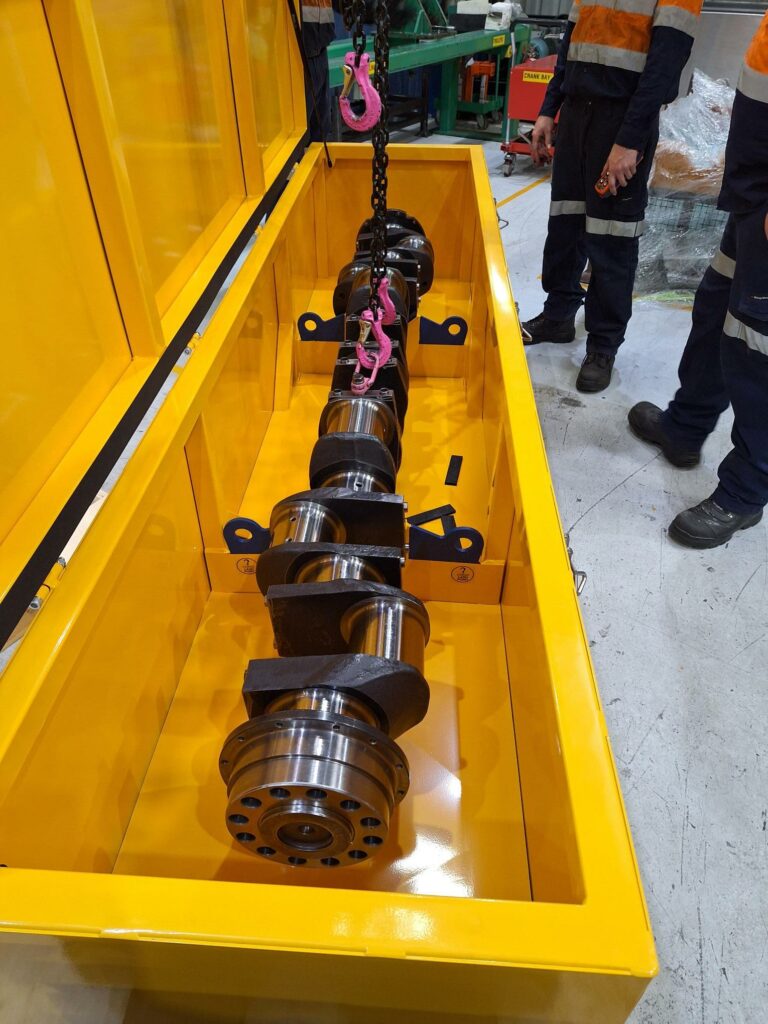
The crankshafts were used three different CAT engine types: the C175-16, 3516 and 3512. The solution needed to do more than simply hold the crankshafts. It needed to protect them from the elements, accommodate different component configurations and make day-to-day handling easier for workshop teams.
The cost of damage to the crankshaft could quickly extend beyond component repairs and replacement costs to cause operational delays and dips in productivity. Delays could potentially spiral into significant production losses, with 1000s of tonnes of production capacity at a standstill each day, when the mining machinery is down.
Some challenges with existing boxes included issues with storage space optimisation, transport and CoR compliance, and the breakdown of the existing crankshaft boxes. A compliant, durable and stackable solution was required.
CUSTOM CRANKSHAFT SOLUTIONS
DAYWALK designed and supplied purpose-built crankshaft boxes to provide dedicated protection for these high-value crankshafts. The boxes were engineered to accommodate three different types of CAT crankshaft, with adjustable features allowing the same solution to be configured to suit each application.
The crankshaft boxes were engineered with consideration to the practical requirements of a high-volume mining workshop environment.
Crankshaft box features include:
Adjustable design to accommodate C175-16, 3516 and 3512 CAT crankshafts
Full weather protection to help protect high-value components during storage
2-high stackable design, reducing the floor space required for storage by up to 50%
Forkliftable from two sides to ensure flexible handling and positioning
Pallet jack access, so workshop teams can quickly move the crankshaft boxes where required
Purpose-built to reduce the risk of damage during storage and handling
The old frame and box required an update; it needed to provide more protection for the crankshaft and optimise the use of floor space.
DAYWALK’s storage box provided complete protection for the crankshaft with a stackable design to maximise floor space.